If you’re reading this, chances are you’re deep in the manufacturing grind—spent three hours troubleshooting a bottleneck because your CNC machining center is doing its own thing, your 3D printer’s cranking parts in another room, and your quality control station is feeding data on a random Excel sheet you keep emailing to yourself. Sound familiar? I’m Jake, and I run a CNC machining center supply company—we’ve been helping shops like yours stop working in silos for the last seven years, so today we’re talking about the big one: Can a CNC machining center actually play nice with every other piece of equipment on your floor? Spoiler alert: It’s not just possible—it’s what’s going to keep your shop competitive when the next supply chain curveball hits. CNC Machining Center
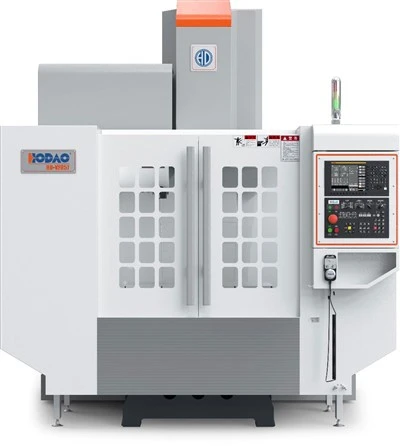
Let’s start with the basics, no tech jargon promised. Most people think a CNC machine is just a big metal box that cuts parts all day. But here’s the thing: modern CNC machining centers aren’t standalone tools—they’re data hubs. Think of it like your phone. Back in the day, your phone only made calls and sent texts. Now it connects to your laptop, your watch, your car, even your coffee maker. That’s exactly how CNC integration works. A few years ago, if you wanted to link your CNC machine to a robotic arm, you’d have to hire a $150-an-hour engineer who’d spend a week wiring cables and writing custom code that would break if you so much as updated your CNC’s software. Now? We’re talking about plug-and-play setups, standard data protocols, and systems that talk to each other like coworkers who actually communicate instead of passive-aggressively leaving sticky notes.
Wait, let’s break down a real example because generic stuff doesn’t help anyone. I had a client last year—small aerospace shop in Detroit, 12 people, making small turbine components. They were using a Haas CNC (we supply most of their machines, so I saw firsthand their pain) and a pair of robotic load/unload arms from a different brand. Before integration, their operators had to manually load raw billets into the CNC, wait for it to finish, unload the finished part, then move it to a coordinate measuring machine (CMM) for QC. That was two minutes of downtime per part, 800 parts a week, so 26 hours of wasted labor a month—no wonder they were working 10-hour days just to hit deadlines. We integrated their CNC with the robots and the CMM in three days. Here’s how it works now: the CMM sends a signal to the CNC that a raw billet is ready. The robot grabs it, loads it into the CNC, runs the pre-programmed machining sequence, then sends a signal to the CMM as soon as the part is done. The CMM scans it, checks for specs, and if it’s good, sends it to the next station for assembly. If it’s bad? It sends a flag to the CNC to adjust its cutting path for the next part. No manual steps, no downtime, operators can now focus on tweaking programs instead of babysitting machines. That’s integration.
But wait, what if you’re not dealing with aerospace? What if you’re a job shop making custom automotive parts, or a medical device maker, or even a small batch woodworking shop? Integration isn’t one-size-fits-all, which is why we work with clients to build systems that fit their specific setup. Let’s talk about common equipment pairs that work seamlessly with CNC machining centers: robotic material handling (load/unload arms, AGVs that move parts between stations), CMMs and vision systems for QC, 3D printers for making custom fixtures or prototype parts, ERP and MES software (think of these as your shop’s command center) that pulls orders, sends program updates to the CNC, and tracks production in real time. The key here is that most modern equipment now uses standard communication protocols—like MTConnect, OPC UA, or even just simple APIs. A lot of old-timers in manufacturing will tell you “old machines can’t integrate,” and yeah, if your CNC is from 1998 with a 5-inch CRT screen, you might need a small retrofitting module to add connectivity. But even that’s not as expensive or complicated as it sounds—we’ve retrofitted 15-year-old CNCs for clients that thought they’d have to replace their entire machine just to link it to their QC station.
Now, let’s get real about the why, because everyone’s asking “what’s in it for me?” First, it cuts downtime. The Detroit shop I mentioned earlier saw a 32% jump in production in the first quarter after integration, no new machines, no new hires. Second, it reduces human error. When a robot loads a part, it’s consistent—no operator forgetting to clamp a billet, no transposing numbers on a part program. That’s huge for medical or aerospace parts, where a tiny error can mean a failed component or a safety hazard. Third, it gives you real-time data. If your CNC is integrated with your MES software, you can see exactly how many parts are being made, how long each operation takes, where the bottlenecks are—all on your phone, all day. Last quarter, a client of ours used that data to find that their CNC was running 15 minutes of downtime every shift because a single tool was wearing out. They swapped out the tool monitoring sensor on their CNC, linked it to their tool crib, and now the crib sends a new tool right to the CNC the second the old one hits a wear limit. That’s $45,000 a year in saved downtime, no joke.
But wait—there are myths out there, right? I hear them all the time when I’m talking to shop owners. Let’s bust the top three. Myth #1: Integration is too expensive for small shops. Yeah, if you’re buying a $500,000 fully automated cell, it’s pricey. But most of our small clients are doing basic integration for under $10,000—robotic load arm, a small MES module, and linking their existing CNC to their CMM. We work with them to phase it in, too—start with linking load/unload, then add QC, then add data tracking. No need to do everything at once. Myth #2: It’s too complicated, we’ll break our workflow. Again, not if you do it right. We have a team of techs that come on-site, train your operators in a half-day, and stay for a week to troubleshoot. Most operators pick it up in a couple days—these aren’t rocket science, they’re just tools that talk to each other. Myth #3: It’s only for big corporations. Look, the Detroit shop I talked about has 12 employees. They make parts for Boeing and Lockheed, but they didn’t have a huge budget. Integration leveled the playing field for them—they can take on bigger contracts because they don’t have to worry about missing deadlines due to manual labor.
Now, let’s talk about what integration actually looks like day-to-day for a shop. Let’s say you’re a job shop making custom motorcycle parts. You get an order for 50 custom engine brackets. You pull it up in your ERP software, which sends the CAD file and machining program straight to your CNC machining center. The CNC alerts your robotic arm that it needs a raw aluminum billet. The arm grabs the billet from the stock area, loads it into the CNC, and locks it in. The CNC runs the program, and every time it’s done with a cut, it checks the tool wear sensor. If the tool is good, it keeps going; if not, it signals the tool crib to send a replacement. When the part is done, the CNC sends it to the vision QC system, which scans the bracket to make sure the holes are the right size, the edges are smooth, and the tolerances are within spec. If it passes, the vision system sends it to the staging area for shipping, and updates the ERP to say “50 brackets, 25 done, 25 left.” If it fails, it sends a flag to the CNC to adjust the cutting path for the next part, and alerts your QC guy to take a look. No one’s standing around, no one’s redoing parts, no one’s emailing files back and forth. That’s not some futuristic factory scene— that’s a shop that’s been integrated for six months, and it’s working.
Wait, but what about when something goes wrong? I’m not here to say integration is perfect. Last year, one of our clients had a power blip, and the connection between their CNC and their robotic arm dropped. The CNC shut down, and the arm was holding a raw billet. It was a 15-minute fix, and they only lost two parts. Without integration, they would have had an operator come in on a weekend to reset the machine, and lost a full shift. So there are growing pains, but they’re way smaller than the pains of working in silos. The key is working with a supplier that offers support—someone that’s not just selling you a CNC machine, but helping you set up the integration, train your team, and be there if something breaks. That’s the difference between us and a lot of big CNC brands, right? We don’t just drop a machine off and vanish. We’re the ones answering calls at 8 PM when the CNC is acting up, and helping you adjust the integration when your shop’s needs change.
Let’s circle back to the original question: Can a CNC machining center be integrated with other manufacturing equipment? The answer is a resounding yes—but it’s not just about connecting cables. It’s about making your shop work smarter, not harder. It’s about cutting downtime, reducing errors, and giving you the data you need to make better decisions. I’ve seen it with my own clients, from the tiny 5-person woodworking shop that integrated their CNC with a laser cutter to cut setup time by 40%, to the medium-sized automotive shop that linked their CNCs to their assembly line to cut production time in half. It’s not some magic trick, it’s just using the tools we have to stop wasting time on stuff that humans shouldn’t have to do, and focus on the stuff that matters—making good parts, growing your business, and not pulling all-nighters just to hit a deadline.
If you’re sitting there thinking, “This sounds like something we could use, but we don’t know where to start,” let’s talk. I’m not gonna pitch you a $100,000 system right off the bat. I’m gonna ask you what your biggest pain points are—are you losing too much time loading parts manually? Are you having a hard time keeping up with quality standards? Are you struggling to track production in real time? Then we’ll build a plan that fits your shop, your budget, and your current equipment. No jargon, no pushy sales talk, just real advice from someone who’s been in this game long enough to know that every shop’s needs are different.
At the end of the day, manufacturing is changing. The shops that adapt are the ones that work together, not in silos. A CNC machining center isn’t just a metal box that cuts parts—it’s the core of a more efficient, profitable shop. Integrate it, and you’re not just keeping up with the competition—you’re getting ahead.
Engraving and Milling Machine References:
- MTConnect Institute. (2023). “Integrating CNC Machining Centers into Smart Manufacturing Environments.” Retrieved from MTConnect official documentation for standard machine-to-machine communication protocols.
- American Machinist. (2022). “Small Shop Integration: How Job Shops Are Leveraging CNC Connectivity to Boost Productivity.” Industry report on mid-sized manufacturing operational efficiency.
- National Institute of Standards and Technology (NIST). (2021). “Manufacturing Integration Guidelines: Connecting CNC Equipment to Robotic Material Handling and Quality Control Systems.” NIST manufacturing extension partnership technical brief.
- Haas Automation. (2023). “CNC Retrofit Options for Older Machines: Enabling Connectivity for Legacy Equipment.” Supplier technical guide for upgrading existing CNC machinery for Industry 4.0 integration.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional CNC machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk CNC machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
